The answer depends less on the maximum theoretical output and more on how you manage operating hours, delivery distance, utilization, material supply, and peak-day demand. For many contractors and concrete producers, a 50 m³/h concrete plant can provide a useful balance between production capacity and investment cost. However, the batching plant should match the actual project schedule rather than simply the highest daily demand.
Start With Daily Concrete Demand, Not Plant Capacity
When customers compare batching plants, they often start with hourly capacity. However, daily demand gives a more useful starting point. A 50 m³/h plant does not need to run for eight hours every day to produce 400 m³.
For smaller projects, a small concrete plant for sale can also be worth comparing when the average demand stays below the peak requirement. The key is to avoid paying for capacity that remains unused for most of the project.
For example, the basic calculation is simple:
| Daily Concrete Demand | Approx. Production Time at 50 m³/h | Practical Meaning |
|---|---|---|
| 200 m³/day | 4 hours | Suitable for a normal production day |
| 250 m³/day | 5 hours | Moderate utilization |
| 300 m³/day | 6 hours | Good utilization for many projects |
| 350 m³/day | 7 hours | Higher utilization with tighter logistics |
| 400 m³/day | 8 hours | Near full planned hourly production |
These figures use the rated production rate as a simple planning reference. Actual output can be lower because of truck availability, aggregate loading, mix design changes, maintenance, traffic, and other site conditions.
Therefore, a contractor should not assume that a 50 m³/h plant will automatically deliver 400 m³ every day. Instead, the key question is whether the plant can cover the project’s normal demand while handling occasional peak days.
Why Variable Demand Does Not Automatically Mean Low Profitability
Variable demand is normal in construction. A project may start with small concrete volumes, move into structural work, and then reach a much higher demand during foundations, columns, slabs, roads, or other large pours.
As a result, the plant’s profitability should be evaluated across the project period rather than based on one low-demand day.
Consider the Average Utilization
Suppose a contractor produces 200 m³ on several days and 400 m³ on several peak days. The plant may still achieve healthy utilization over the month.
For example, imagine a 20-day production month:
- 10 days at 200 m³/day = 2,000 m³
- 6 days at 300 m³/day = 1,800 m³
- 4 days at 400 m³/day = 1,600 m³
- Total monthly production = 5,400 m³
The important point is that the plant does not need to operate at maximum capacity every day. Instead, it needs enough utilization to support the project’s overall concrete requirement and avoid unnecessary idle capacity.
Moreover, producing concrete on demand can reduce dependence on external ready-mix suppliers. This can become particularly relevant when outside suppliers have limited delivery slots, long transport distances, or higher prices during peak construction periods.
Compare the Cost of Owning the Plant With Buying Ready-Mix Concrete
Profitability does not come from production capacity alone. It comes from the difference between the cost of producing concrete and the cost of obtaining the same concrete from another source.
For an internal batching operation, the contractor should consider several cost categories:
- Cement and supplementary materials
- Sand and aggregate
- Water and admixtures
- Electricity or fuel
- Loader or aggregate handling costs
- Plant operators and labor
- Maintenance and spare parts
- Concrete mixer truck operation
- Plant depreciation and financing
At the same time, compare these costs with the delivered price of ready-mix concrete in the project area. The transport component deserves particular attention. If the project is far from commercial batching plants, transportation can significantly affect the delivered concrete cost.
For contractors supplying concrete to several nearby projects, a ready mix batching plant may provide another operating model. Instead of producing only for one construction site, the plant can potentially serve multiple customers, depending on local demand, transportation capacity, and business arrangements.
A Simple Contribution-Margin Calculation
A useful first calculation is:
Concrete contribution margin = external concrete cost per m³ − internal production cost per m³
Then estimate:
Monthly contribution = contribution margin × monthly concrete volume
This number does not represent final profit because fixed costs, financing, depreciation, and other business expenses still matter. However, it helps a contractor understand whether producing concrete internally could create enough value to justify the plant investment.
What Happens When Demand Falls to 200 m³ per Day?
This is where plant sizing becomes important. A contractor does not necessarily need a larger plant simply because the project occasionally reaches 400 m³/day.
At 200 m³/day, a 50 m³/h plant theoretically requires about four hours of production. That leaves time for plant setup, material preparation, cleaning, maintenance, and other site activities.
Therefore, the lower-demand period does not necessarily mean the plant is underutilized to an unacceptable level. In fact, shorter daily production can sometimes help contractors control operating hours and avoid unnecessary equipment running time.
However, the economics change if the project remains close to 200 m³/day for a long period while the plant investment is high. In that situation, the contractor should calculate the actual monthly utilization before purchasing.
Can the Same Plant Handle 400 m³ on Peak Days?
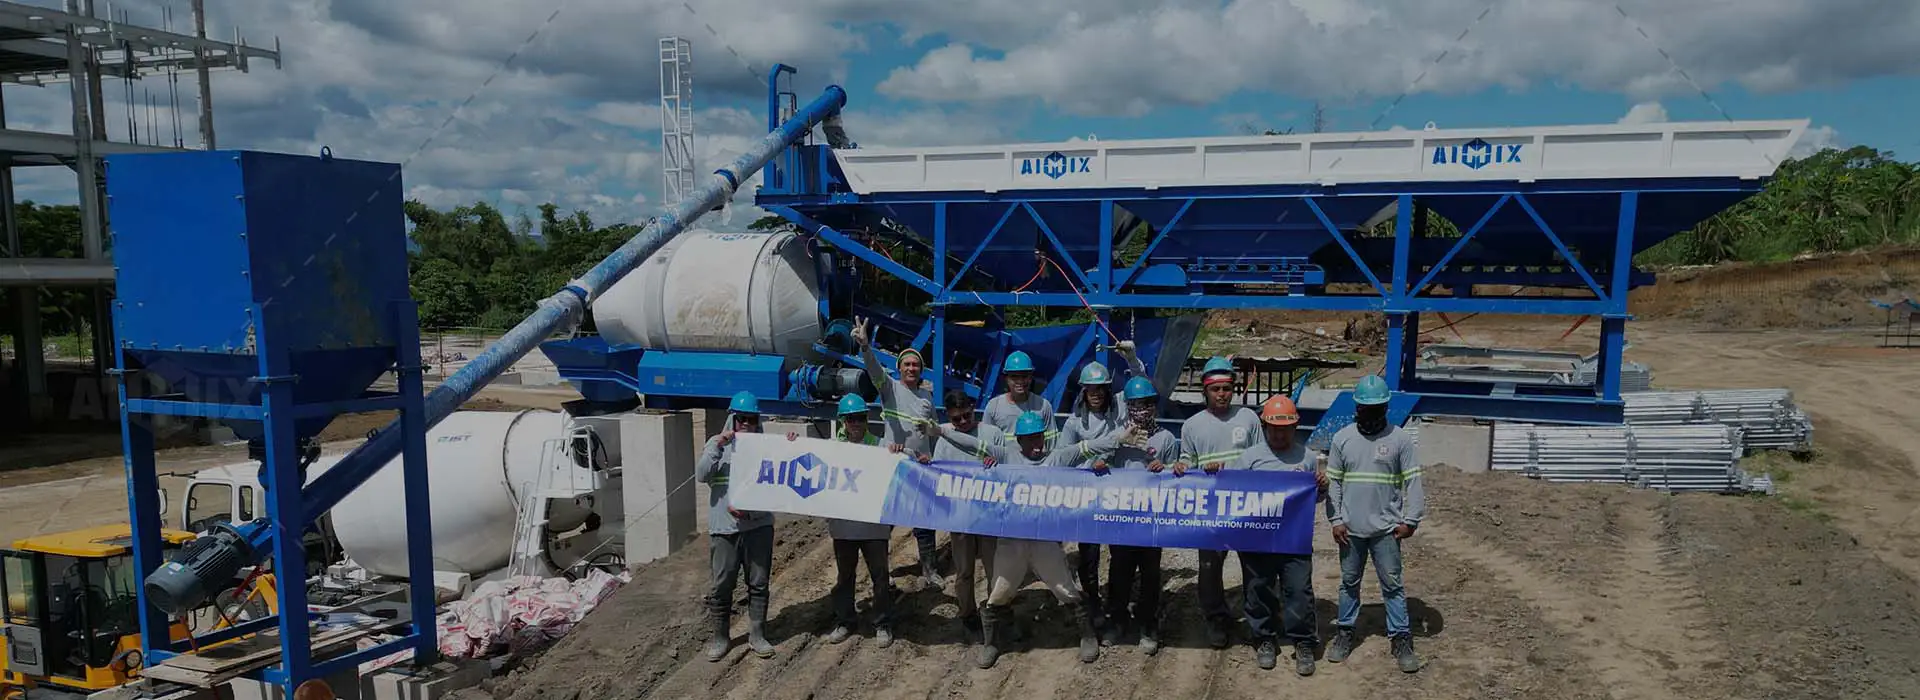
Yes, a 50 m³/h plant can theoretically produce 400 m³ in eight hours of continuous production. But peak-day planning requires more than looking at the batching plant’s rated capacity.
Truck Availability Becomes Critical
The batching plant can only maintain production if mixer trucks can continuously receive and transport concrete.
If each truck carries 8 m³, producing 400 m³ means approximately:
400 ÷ 8 = 50 truckloads
That does not mean you need 50 trucks. The required fleet depends on the round-trip cycle time. Loading, traveling, unloading, and returning all affect how many trucks can keep the plant working.
Therefore, a contractor with a 50 m³/h plant should calculate truck cycle time before scheduling a 400 m³ pour. Otherwise, the batching plant may spend part of the day waiting for trucks.
Project Location Can Change the Profitability Calculation
Distance is another major factor. A batching plant close to the construction site can reduce concrete transportation time. This becomes increasingly important when daily demand reaches 300–400 m³.
For remote projects, islands, infrastructure projects, resorts, industrial sites, and large developments, producing concrete closer to the point of use can offer operational advantages.
For smaller construction sites with limited space, a mini batching plant indonesia option may also be considered. Its suitability depends on the project’s required output, available installation area, aggregate storage, and expected operating period.
For example, if commercial ready-mix suppliers are located far from the project, long delivery cycles can create scheduling problems. Concrete trucks may spend more time on the road instead of serving the project.
By contrast, an on-site or nearby batching plant can shorten the supply chain. Consequently, the contractor gains more control over production timing.
When Should You Consider a 50 m³/h Plant?
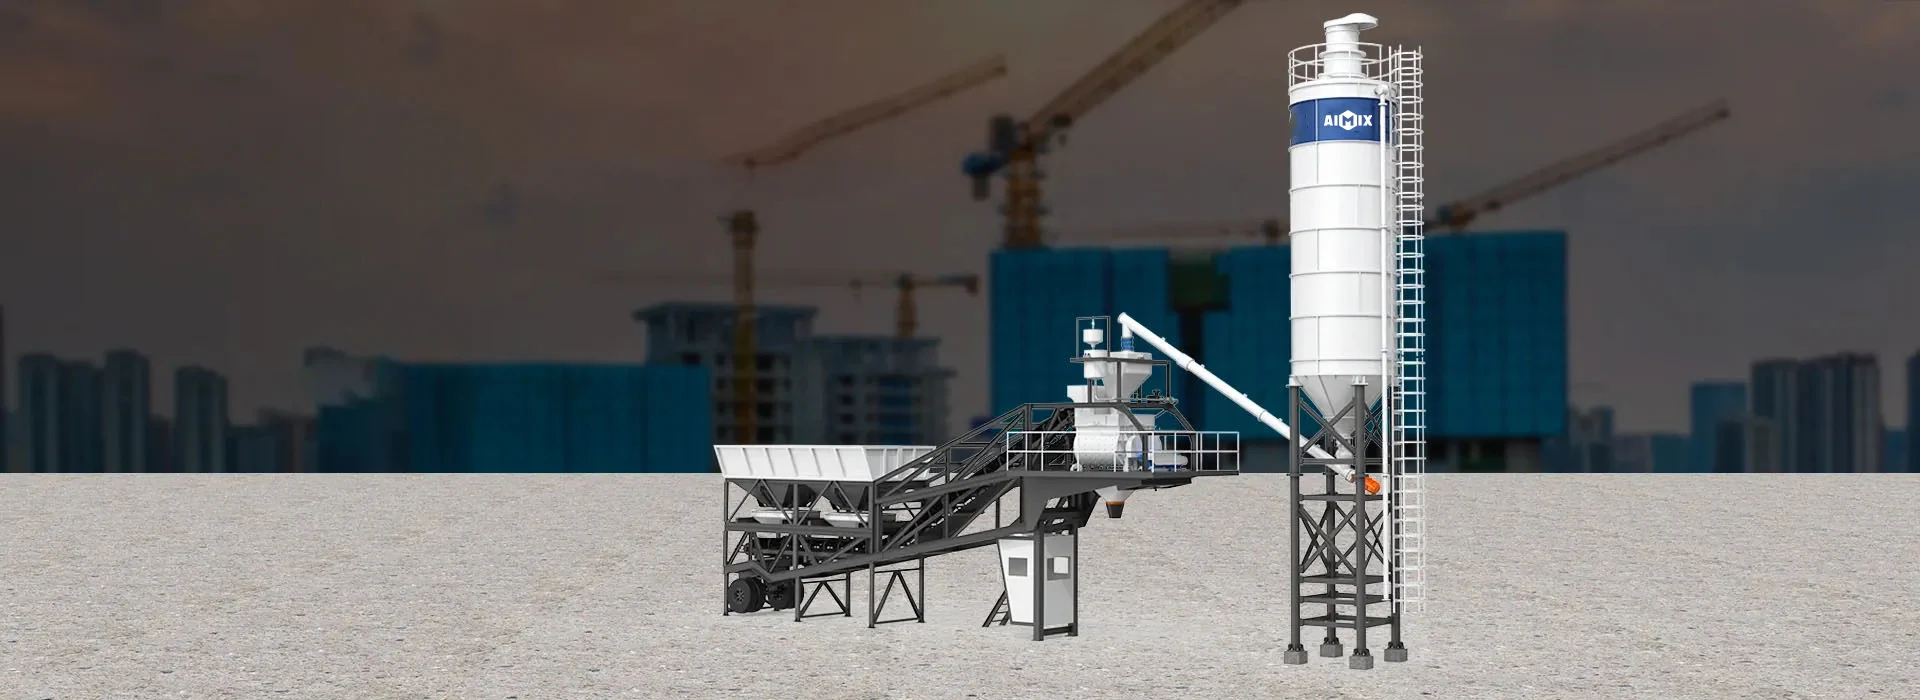
A 50 m³/h plant can fit projects with changing demand when several conditions align.
- Normal demand is around 200–300 m³/day.
- Peak demand can reach approximately 400 m³/day.
- The project lasts long enough to justify the equipment investment.
- Concrete delivery from external suppliers is expensive or unreliable.
- The contractor has sufficient mixer trucks or access to them.
- Aggregate, cement, water, and admixtures can be supplied consistently.
- The project requires regular concrete production rather than occasional small pours.
These conditions are more important than simply choosing a plant because its rated capacity looks attractive. The contractor should also compare different batching plant beton configurations based on output, site conditions, material handling, automation, and future utilization.
When Could a Larger Plant Make More Sense?
A 50 m³/h plant may not be the right capacity for every project. If 400 m³/day becomes the normal requirement rather than an occasional peak, the contractor should also compare higher-capacity options.
For example, a project with several consecutive 500–600 m³ pours may need a different production strategy. A larger plant could reduce the number of operating hours needed to meet the same daily demand.
However, higher capacity also means higher equipment investment and potentially greater supporting requirements. These can include aggregate storage, cement storage, loading equipment, power supply, mixer truck fleets, and site space.
Therefore, bigger is not automatically better. The right capacity should reflect the relationship between average demand, peak demand, project duration, and total operating cost.
Use a Peak-Day Strategy Instead of Oversizing the Plant
One practical approach is to size the batching plant around regular demand while planning logistics around peak pours.
For a project that usually consumes 200–300 m³/day but occasionally reaches 400 m³, the contractor can focus on keeping the 50 m³/h plant well supplied and coordinating the mixer truck fleet during peak periods.
In addition, accurate production scheduling can reduce waiting time. The site team can prepare reinforcement, formwork, access routes, aggregate, cement, and trucks before the concrete pour begins.
As a result, the plant spends more time producing concrete instead of waiting for the next step in the process.
Build a Project-Specific Profitability Model
Before making the investment, contractors should build a simple model using their own project data. Generic prices cannot replace local numbers.
| Input | Question to Check |
|---|---|
| Concrete demand | What is the average and peak m³/day? |
| Project duration | How many months will the plant operate? |
| Concrete price | What is the delivered local ready-mix price? |
| Material cost | What is the actual cost per m³ for the mix design? |
| Transport | How far is the project from external suppliers? |
| Plant investment | What is the total purchase and installation cost? |
| Truck fleet | How many trucks are needed for the planned cycle time? |
| Utilization | How many hours per day and days per month will the plant run? |
Once these figures are available, the contractor can estimate monthly production, operating cost, savings compared with purchased concrete, and the investment recovery period.
Conclusion: Look at the Whole Concrete Supply Chain
A 50 m³/h batching plant can be a practical option for projects where concrete demand moves between 200 and 400 m³ per day. At 200 m³/day, the plant has enough capacity to meet demand without requiring a full working day of production. At 400 m³/day, it can theoretically support the required volume within about eight hours of production.
However, profitability depends on the complete operating system. Material prices, ready-mix prices, transport distance, mixer truck cycle time, labor, maintenance, plant utilization, and project duration all influence the final result.
For this reason, the best starting point is not simply asking, “How many cubic meters per hour do I need?” Instead, ask, “How much concrete will I produce, how often will demand peak, and what will each cubic meter cost me?”
If your project demand typically ranges from 200 to 400 m³/day, AIMIX can help you compare batching plant capacity, production schedules, mixer truck requirements, and site conditions. Share your expected daily concrete volume, project duration, location, and peak pouring requirements, and we can work through a practical 50 m³/h batching solution for your project.